Current condition
Define the handover point, required orientation, usable delivery rate and agreed observation method before the trial. Record the part revision, sample group, bulk condition, settings and downstream operating state with each result.
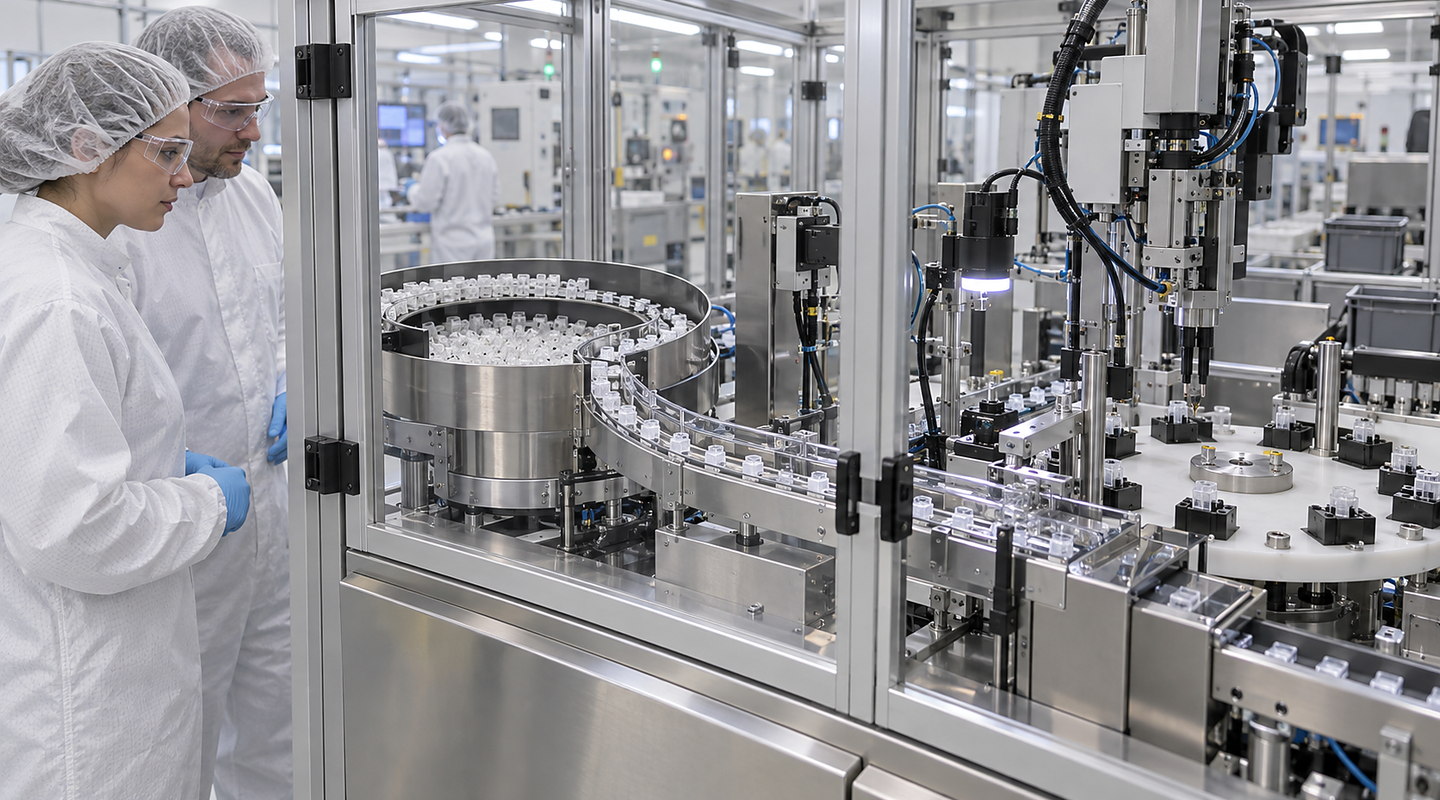
What evidence should be agreed before acceptance testing for syringe part feeders?
Agree acceptance against the correctly oriented, usable components delivered at the downstream handover, with a stated part range, test period and operating conditions. Record jams, damage, mixed-variant observations and recovery separately. Start with the component sample guide.
For bulk presentation using syringe-component feeding and orientation, describe the realistic range and how changes in jam, damage and recovery acceptance checks affect the result you need.
Plan syringe part feeders around real component variation, bulk condition, orientation, usable delivery rate and the downstream interface. Discuss representative part trials with Sorting Solutions. Use this guide to resolve jam, damage and recovery acceptance checks before it limits the final system.
Discuss your application

Define the handover point, required orientation, usable delivery rate and agreed observation method before the trial. Record the part revision, sample group, bulk condition, settings and downstream operating state with each result.
Cover the agreed normal, marginal and supplier-variant components, replenishment conditions, short stops and variant changes. Keep cases outside that tested range clearly identified; a successful nominal run does not demonstrate them.
For each agreed jam, damage, wrong-orientation or mixed-variant scenario, define the expected response, responsible person and approved recovery method. Record the first usable output after restart and any unresolved action.
Identify every component variant and drawing revision in the test record. Keep normal, marginal and supplier-variant samples distinguishable so the result can be traced to the range actually tried.
Compare component condition before and after feeding against the agreed critical surfaces and permitted contact areas. The responsible manufacturer defines handling and cleanliness requirements; a feeding trial alone does not establish product release or validation.
Record the bulk condition, replenishment method and operating state during each trial. Include the agreed replenishment and interruption cases in the result record rather than describing automatic running alone.
Count correctly oriented, usable deliveries at the agreed downstream handover over the stated period. Report stops, interventions and unusable deliveries separately so nominal feeder output is not presented as usable production rate.
Record the transfer position, downstream ready conditions and the agreed response when the next process cannot accept a component. Check the actual handover rather than treating arrival at the feeder outlet as proof of downstream use.
Keep a record of the agreed fault scenario, observed response, safe intervention and restart. Separate accepted results, failures, untested conditions and actions still open before agreeing the handover scope.